The precision and reliability of fluid control systems often depend on the smallest components, where a high-quality 10mm ball valve plays a pivotal role. In the complex landscape of industrial piping, the ability to achieve a tight, leak-proof seal while maintaining low fluid resistance is essential for operational safety and efficiency. These components are engineered to handle the rigorous demands of modern manufacturing, ensuring that media flow is managed with absolute precision.
Globally, the demand for specialized valves has surged as industries transition toward more corrosive media and higher pressure environments. Whether integrated into water treatment plants or chemical processing lines, the implementation of a robust 10mm ball valve addresses the critical challenge of preventing unplanned downtime caused by seal failure. By utilizing advanced materials and a simplified two-piece design, these valves offer a balanced solution for both high-performance requirements and ease of maintenance.
Understanding the technical nuances of the 10mm ball valve allows engineers to optimize their systems for longevity and safety. From the selection of RPTFE seats for heat resistance to the choice of acid-resistant alloys, every detail contributes to the valve's ability to function in extreme temperatures and pressures. This guide explores the structural advantages and industrial applications that make this specific valve a cornerstone of fluid control.
Technical Design of the 10mm Ball Valve
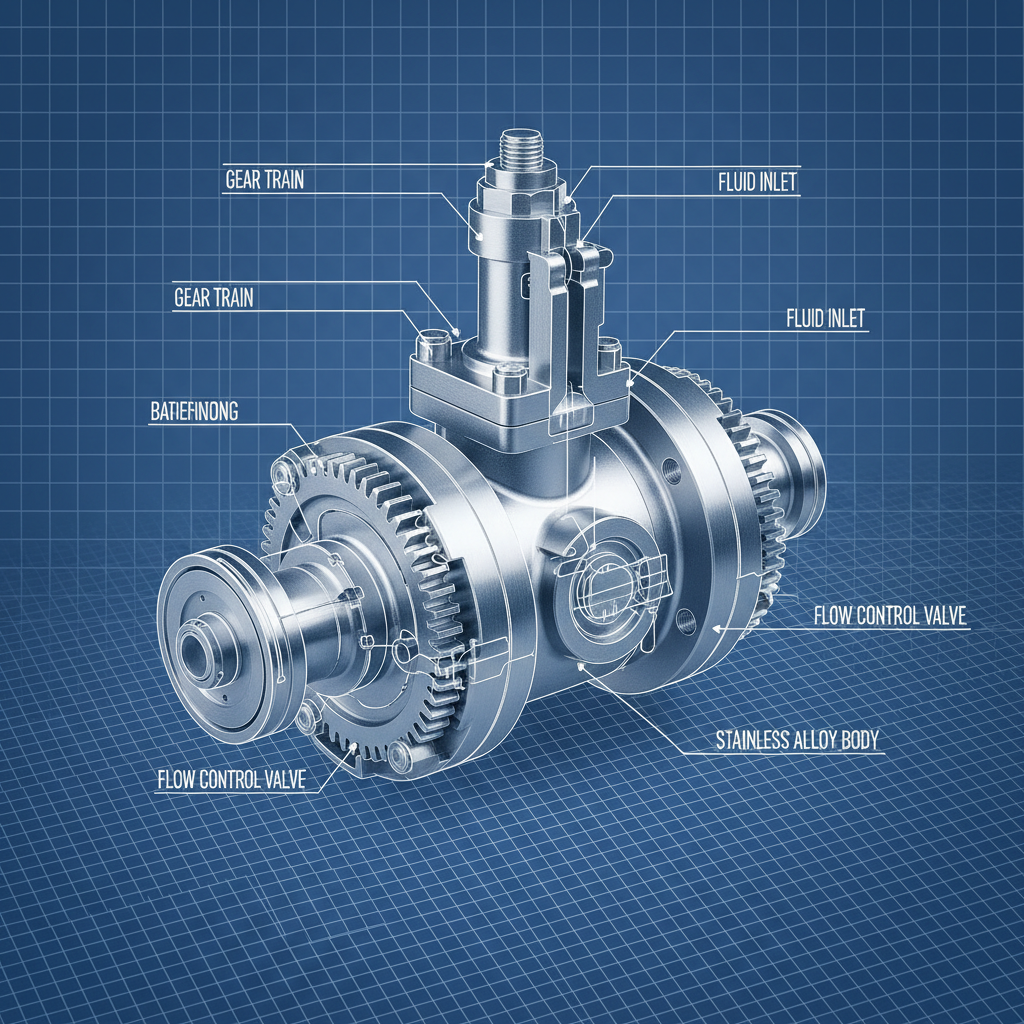
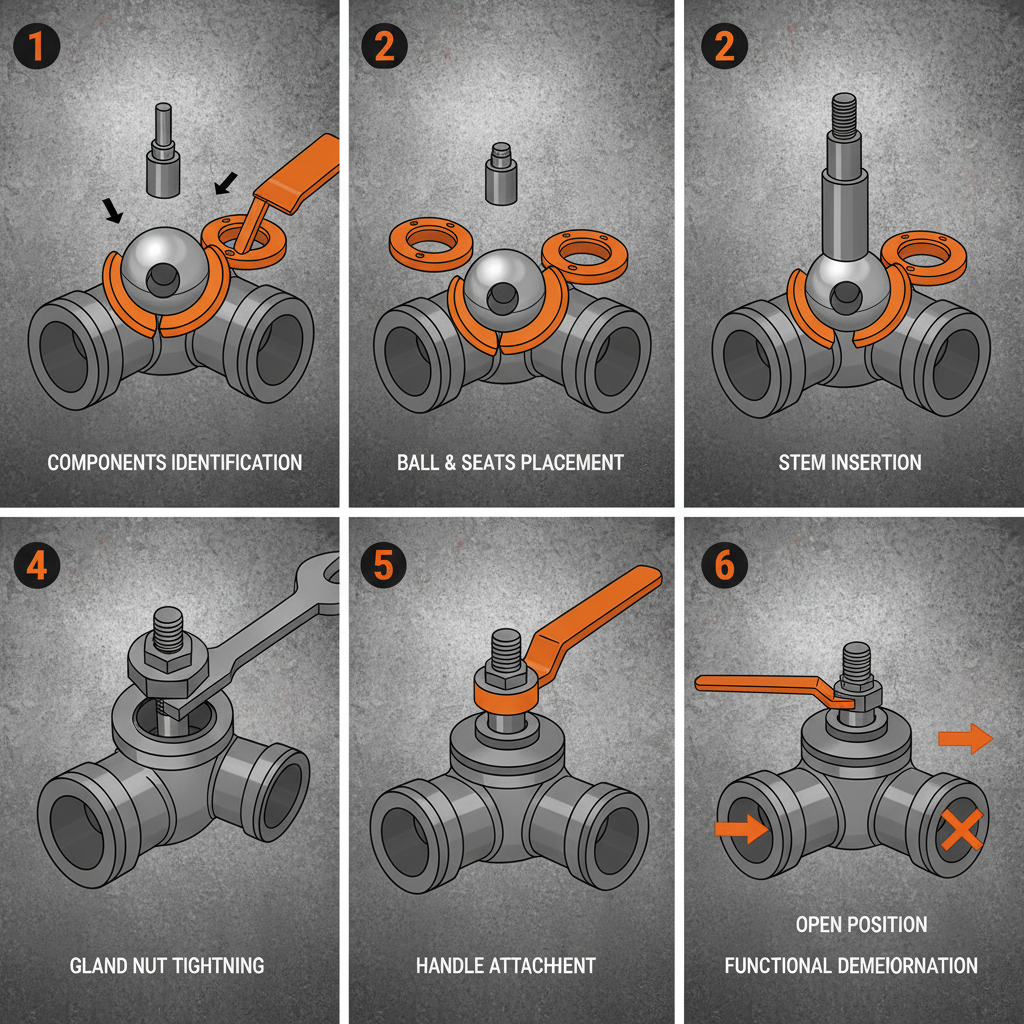
The 10mm ball valve utilizes a sophisticated two-piece design featuring a spherical body with a circular channel. This geometry allows the ball to rotate in synchronization with the valve stem, creating an efficient mechanism for opening and closing the flow path. Because the spherical surface provides a tight seal against the seats, it effectively cuts off or connects the medium within the pipeline without significant pressure drops.
Beyond simple on-off functionality, this design is optimized for regulation and fluid control. Its compact size and light weight make it an ideal choice for equipment with limited spatial footprints, while the low fluid resistance ensures that the energy required to move liquids or gases is minimized. This structural simplicity not only enhances reliability but also reduces the potential for erosion on the sealing surfaces.
Material Superiority and Corrosion Resistance
A critical advantage of the 10mm ball valve lies in its use of RPTFE (Reinforced Polytetrafluoroethylene) ball seats. Compared to standard PTFE, RPTFE offers significantly higher intensity and superior heat resistance, making it suitable for volatile environments. Options such as PTFE infused with 25% carbon or SS316 reinforcements further enhance the valve's ability to withstand mechanical wear and thermal expansion.
The structural materials are engineered to meet strict international standards, ensuring a high degree of resistance to both acids and alkalis. This makes the valve an indispensable tool when dealing with corrosive gases and liquids that would typically degrade lower-grade components. The chemical inertness of the materials prevents contamination of the medium and protects the integrity of the pipeline.
By combining these high-performance polymers with corrosion-resistant metals, the valve maintains a reliable seal even under challenging conditions. This material synergy ensures that the 10mm ball valve remains operational in industries where chemical aggression is a constant threat, reducing the frequency of replacements and increasing overall plant safety.
Performance Factors in Fluid Dynamics
The fluid dynamics of a 10mm ball valve are characterized by a "full bore" or "near full bore" flow path, which minimizes turbulence. This ensures that the medium passes through the valve with minimal friction, effectively reducing the energy loss associated with pressure drops in high-velocity systems.
Reliability in sealing is the most critical performance factor. The precision-machined spherical body of the 10mm ball valve ensures that when the valve is closed, the contact between the ball and the RPTFE seat is absolute, preventing any leakage of hazardous or expensive fluids.
Furthermore, the valve is designed to operate across a wide spectrum of temperatures. Whether facing the extreme heat of a steam line or the cryogenic temperatures of certain chemical processes, the material stability of the 10mm ball valve prevents deformation, ensuring the valve remains easy to operate.
Operational Efficiency and Reliability
Operational efficiency is achieved through the simplicity of the quarter-turn mechanism. A 90-degree rotation of the handle provides a complete transition from fully open to fully closed, allowing operators to react quickly in emergency shut-off scenarios. This rapid response time is a key safety feature when managing high-pressure liquids or gases.
The long-term reliability of the 10mm ball valve is attributed to its resistance to erosion. Unlike globe valves where the fluid may wear down the seat over time, the ball valve's sealing surface is designed to withstand the constant flow of abrasive media without losing its integrity.
Operational Performance Metrics for 10mm Ball Valve Variants
Global Industrial Applications
The versatility of the 10mm ball valve makes it widely applicable across various global sectors. In water treatment facilities, these valves manage the flow of purification chemicals and filtered water, ensuring precise dosing and flow control. Similarly, in the petroleum and natural gas industry, they are used in sampling systems and instrumentation lines where a reliable seal is paramount to prevent leaks.
Chemical manufacturing plants rely on these valves to handle corrosive acids and alkalis, while heating systems use them to regulate thermal fluids. Because they can withstand high pressures and temperature extremes, they are equally effective in remote industrial zones and high-tech urban infrastructure, providing a dependable solution for fluid management.
Installation and Maintenance Best Practices
Correct installation is fundamental to the lifespan of a 10mm ball valve. It is highly recommended to install the valve in a horizontal position. This orientation ensures that the ball rotates smoothly and reduces the impact of gravity on the internal components, which prevents premature wear and ensures a more consistent seal over thousands of cycles.
Regular maintenance is the second pillar of operational longevity. Technicians should conduct periodic checks to verify the sealing integrity and the flexibility of the handle operation. Any resistance in the rotation may indicate the accumulation of debris or the beginning of seat degradation, necessitating a prompt cleaning or inspection.
To further extend service life, it is essential to keep both the interior and exterior of the valve clean. Removing external contaminants prevents stem leaks, while internal flushing removes particulates that could scratch the spherical surface of the ball. Following these simple steps ensures the valve performs at peak efficiency for years.
Comparative Analysis of Valve Specifications
When selecting a 10mm ball valve, engineers must compare the technical specifications against the operational environment. The choice between different RPTFE seat variations, such as carbon-filled versus stainless steel reinforced, depends on whether the primary threat is heat, mechanical abrasion, or chemical corrosion.
Weight and size also play a critical role in system design. The lightweight nature of the two-piece construction allows for easier installation in tight spaces, reducing the load on supporting piping. This is particularly important in modular equipment where every gram of weight affects the overall system footprint.
Ultimately, the value of the valve is measured by its total cost of ownership. While premium materials may have a higher initial cost, the reduction in maintenance frequency and the prevention of costly leaks make high-spec ball valves the more economical choice in the long run.
Technical Specifications Comparison for 10mm Ball Valve Configurations
| Seat Material |
Heat Resistance |
Corrosion Grade |
Durability Score |
| PTFE+25% Carbon |
Very High |
Excellent |
9/10 |
| PTFE+SS316 |
High |
Superior |
10/10 |
| Standard RPTFE |
Medium-High |
High |
8/10 |
| Pure PTFE |
Medium |
High |
6/10 |
| Glass-filled PTFE |
High |
Medium-High |
7/10 |
| Composite Polymer |
Medium |
Medium |
5/10 |
FAQS
The 2-piece design offers a superior balance between compact size and ease of maintenance. It provides a tight and reliable seal with low fluid resistance, making it more efficient for cutting off or connecting media in pipelines compared to more complex multi-piece valves. Additionally, it is lighter and simpler to install.
RPTFE (Reinforced PTFE) provides higher mechanical intensity and better heat resistance than standard PTFE. When reinforced with carbon or SS316, it prevents the seat from deforming under high temperatures or pressures, ensuring the valve maintains a leak-proof seal even in corrosive industrial environments.
Yes, provided the materials meet international standards for acid and alkali resistance. The use of high-grade alloys and RPTFE seats allows these valves to handle corrosive gases and liquids effectively, making them suitable for chemical manufacturing and petroleum processing.
It is strongly recommended to install the 10mm ball valve in a horizontal position. This ensures smooth rotation of the internal ball and reduces uneven wear on the seats, which helps maintain the valve's operational flexibility and extends its overall service life.
Maintenance frequency depends on the medium and environment, but regular checks for sealing integrity and operational flexibility are essential. Cleaning the interior and exterior of the valve periodically prevents the buildup of contaminants and ensures the valve opens and closes smoothly.
Yes, especially the versions equipped with carbon-filled or SS316 reinforced RPTFE seats. These materials are specifically designed to handle higher temperatures without losing their sealing properties, making them ideal for heating systems and high-temperature industrial applications.
Conclusion
The 10mm ball valve stands as a critical component in modern fluid control, blending technical simplicity with high-performance materials. By leveraging the strengths of RPTFE seats and a precision two-piece design, it addresses the industry's need for low-resistance, corrosion-resistant, and highly reliable flow management. From its ability to operate in extreme temperatures to its ease of maintenance, the valve provides tangible value across the water treatment, chemical, and petroleum sectors.
As industrial processes move toward greater automation and more aggressive chemical environments, the importance of utilizing high-specification valves becomes even more evident. Investing in quality materials and adhering to strict installation and maintenance protocols will ensure long-term system stability and safety. For those seeking to optimize their fluid control infrastructure, exploring specialized ball valve solutions is the most effective path forward. Visit our website for more information: www.houdevalve.com