The industrial landscape relies heavily on precise fluid control to ensure safety and efficiency across various sectors. Among the most critical components in these systems is the 10 ball valve, a high-performance tool designed for durability and seamless operation in demanding environments. Understanding the technical nuances of these valves is essential for engineers aiming to minimize downtime and maximize system longevity.
Global demand for robust valve solutions has surged as industries shift toward more corrosive media and extreme temperature ranges. The 10 ball valve addresses these challenges by combining advanced material science with a streamlined structural design, effectively eliminating common failure points found in multi-piece assemblies. This evolution in manufacturing ensures that critical pipelines remain secure and leak-free.
Whether utilized in large-scale chemical processing or municipal water treatment, the 10 ball valve provides an economical yet industrial-grade solution. By integrating high-quality PTFE seals and corrosion-resistant bodies, these valves offer the versatility required to handle everything from compressed air to high-purity chemicals.
Structural Integrity of the 10 Ball Valve
The architectural core of the 10 ball valve lies in its integrated one-piece body design. Unlike traditional multi-part valves, this unified construction eliminates several potential leakage paths, significantly enhancing the overall structural integrity of the fluid control system. This design choice not only boosts reliability under high pressure but also simplifies the installation process for field technicians.
Beyond leakage prevention, the compact nature of this design reduces the overall weight of the assembly without compromising strength. This makes the 10 ball valve an ideal choice for complex piping networks where space is limited and lightweight, high-performance components are required to reduce the load on support structures.
Material Excellence and Corrosion Resistance
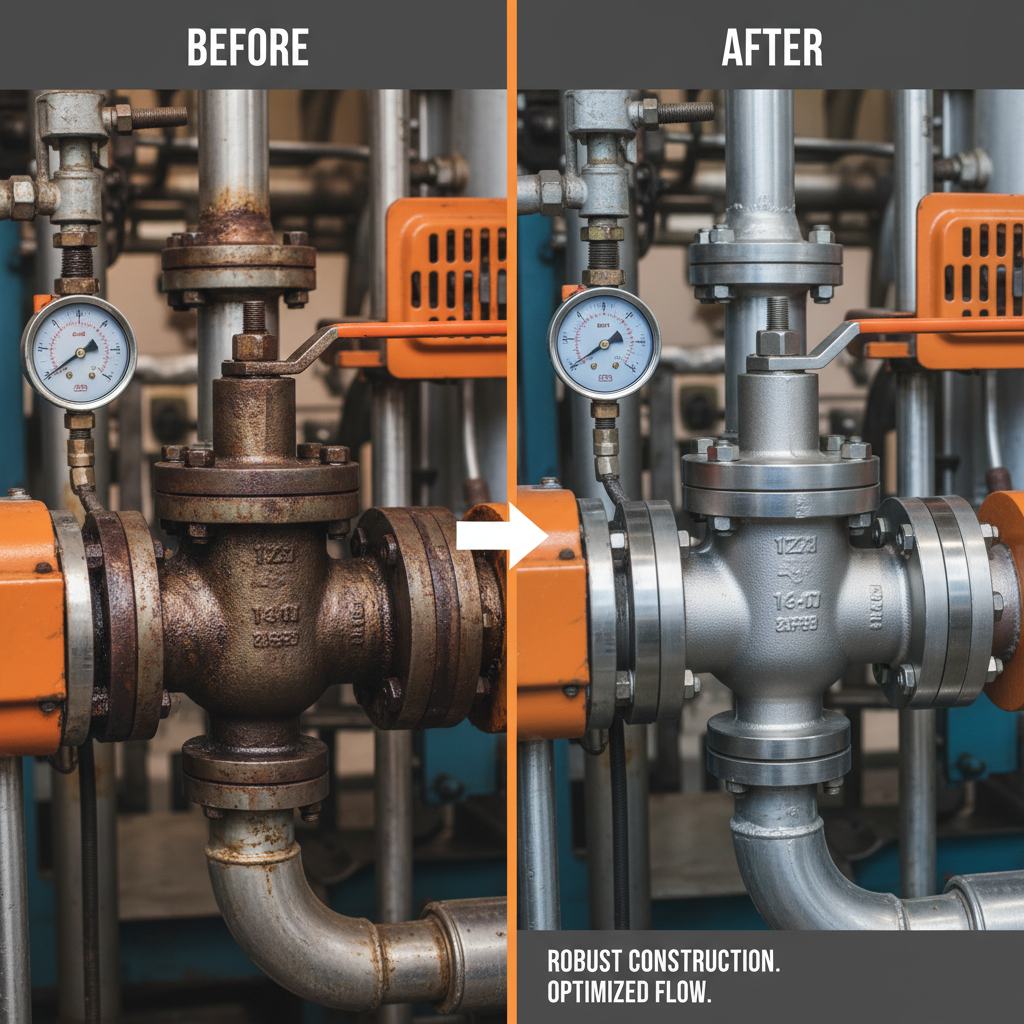
To withstand the rigors of industrial environments, the 10 ball valve is engineered with high-grade materials that prioritize corrosion resistance. This is particularly critical in applications involving saltwater, acidic chemicals, or volatile organic compounds where standard carbon steel would fail rapidly.
The use of premium stainless steel ensures that the valve remains operational even when exposed to harsh external atmospheres or aggressive internal media. This material choice prevents pitting and oxidation, which are the leading causes of valve failure and unplanned system shutdowns in chemical processing plants.
By focusing on material purity and precise alloying, the 10 ball valve maintains its mechanical properties across a wide range of operational stresses. This longevity reduces the total cost of ownership by extending the replacement cycle and ensuring consistent flow control.
Sealing Technology and Temperature Range
The efficacy of any 10 ball valve is largely determined by its sealing mechanism. High-quality PTFE seals are utilized to create a tight, bubble-tight closure that prevents medium escape, ensuring zero leakage performance in suitable pressure environments.
One of the standout features of the 10 ball valve is its wide temperature compatibility. The PTFE components allow the valve to operate reliably from -20°C to 200°C (-4°F to 392°F), making it suitable for both cryogenic-adjacent applications and high-heat industrial steam lines.
Moreover, the low-torque operation provided by these advanced seals means that the 10 ball valve can be opened and closed with minimal effort. This reduces wear and tear on the actuator or handle, further contributing to the device's overall lifespan.
Performance Metrics and Flow Optimization
Optimizing flow is critical to preventing pressure drops within a pipeline. The 10 ball valve is available in both full bore and reduced bore configurations to meet specific project requirements. Full bore options are ideal for applications requiring maximum flow capacity and minimal turbulence.
Conversely, reduced bore configurations allow for more precise flow control and a more compact footprint, which can be advantageous in complex HVAC or irrigation systems where space is at a premium.
10 Ball Valve Configuration Performance Comparison
Global Industrial Applications
The versatility of the 10 ball valve makes it a staple in oil and gas pipelines and chemical processing plants worldwide. In these sectors, the ability to handle corrosive media while maintaining a zero-leakage seal is paramount for environmental safety and operational efficiency.
Beyond heavy industry, these valves are extensively used in water treatment facilities for drinking water and wastewater management, as well as in ship systems where saltwater corrosion is a constant threat. Their reliability ensures that critical utility services remain uninterrupted across different geographic regions.
Long-Term Value and Maintenance Benefits
From a procurement perspective, the 10 ball valve offers significant economic advantages. The one-piece design reduces the number of parts that can fail, which in turn lowers the frequency of maintenance intervals and reduces the need for expensive on-site repairs.
Installation is streamlined due to the compact and lightweight design, allowing engineers to deploy these valves quickly across large-scale irrigation or compressed air systems. This ease of installation translates directly into lower labor costs during the construction phase of a project.
The long service life afforded by sturdy construction and high-grade PTFE seals ensures that the 10 ball valve remains a reliable asset for years, providing peace of mind to operators who prioritize safety and system uptime over the lowest initial purchase price.
Future Trends in Valve Engineering
As the world moves toward greener energy and digital transformation, the 10 ball valve is evolving to integrate with smart monitoring systems. Future iterations are expected to incorporate sensors that can detect wear or leakage in real-time, enabling predictive maintenance and reducing the risk of catastrophic failure.
Sustainability is also driving the adoption of new materials that maintain the high performance of the 10 ball valve while reducing the carbon footprint of the manufacturing process. The shift toward more eco-friendly production methods is becoming a priority for global procurement experts.
Furthermore, automation is playing a larger role, with the 10 ball valve being increasingly paired with intelligent actuators. This allows for remote control and precise modulation of fluid flow, which is essential for the next generation of automated chemical plants and smart city water grids.
Comparison of 10 Ball Valve Specifications and Application Suitability
| Configuration Type |
Primary Benefit |
Recommended Industry |
Durability Rating |
| Full Bore 10 Ball Valve |
Max Flow, Low Pressure Drop |
Oil & Gas Pipelines |
10/10 |
| Reduced Bore 10 Ball Valve |
Compact Size, Cost Effective |
HVAC / Irrigation |
8/10 |
| Stainless Steel Body |
High Corrosion Resistance |
Chemical Processing |
10/10 |
| PTFE Sealed 10 Ball Valve |
Wide Temp Compatibility |
Power Generation |
9/10 |
| One-Piece Design |
Zero Leakage Paths |
Water Treatment |
9/10 |
| Custom Config Valve |
Tailored System Integration |
Specialized Lab Equipment |
9/10 |
FAQS
The primary advantage is the elimination of potential leakage paths. By integrating the body into a single piece, the 10 ball valve removes joints where seals could fail, thereby enhancing structural integrity and significantly reducing the maintenance required to prevent leaks in high-pressure industrial environments.
Yes, thanks to the use of high-quality PTFE seals, this specific 10 ball valve is designed for wide temperature compatibility ranging from -20°C to 200°C. This makes it highly versatile for applications involving both chilled fluids and high-temperature industrial steam.
Absolutely. The valve is engineered with outstanding corrosion resistance, making it ideal for chemical processing and water treatment. The combination of a stainless steel body and PTFE seals ensures longevity when exposed to aggressive media that would typically erode standard valves.
A full bore 10 ball valve has an internal diameter equal to the pipeline, minimizing pressure loss and maximizing flow. A reduced bore valve has a smaller opening, which is used to optimize flow control and reduce the overall size and cost of the valve assembly.
To ensure safe transportation, each 10 ball valve is individually wrapped in anti-corrosion material. They are then packed in strong cardboard boxes or secured on veneer pallets, preventing any physical damage or environmental degradation during transit to global sites.
Yes, custom configurations and certification services are available upon request. Whether you need specific material grades or unique port dimensions, the 10 ball valve can be tailored to meet the exact technical specifications of your industrial project.
Conclusion
The 10 ball valve represents a critical intersection of durability, efficiency, and cost-effectiveness in modern fluid control. By leveraging a one-piece integrated design and high-performance PTFE seals, it provides a reliable solution for the most demanding industrial environments, from chemical processing to water treatment. Its ability to withstand extreme temperatures and corrosive media ensures that it remains a top choice for engineers prioritizing system safety and long-term reliability.
Looking forward, the integration of smart technology and sustainable manufacturing will only enhance the value of these components. For procurement experts and system designers, investing in high-grade valves is not just about immediate functionality, but about ensuring the future resilience of industrial infrastructure. To explore our full range of high-performance solutions, visit our website: www.houdevalve.com.